Custom welded counterweights for reach stackers and port handling equipment — engineered to your drawing as a welded box, so there is no size ceiling to design around.
A reach stacker counterweight is large, heavy, and often still being developed. That combination is exactly where welded fabrication wins.
The box is filled with compacted steel sand at 4.8 t/m³ — roughly double the density of concrete-filled counterweights, so the same weight fits in about half the volume. More on cast-to-welded conversion.
Already running a cast counterweight? We re-engineer it as a welded fabrication — no tooling to pay for, no minimum batch, and no pattern lead time. On a part the size of a reach stacker counterweight, that is usually where the largest saving sits.
Applied across: forklifts · tow tractors · aerial work platforms · reach stackers
How does a welded box match the weight of a casting? The shell is filled with compacted steel sand at 4.8 t/m³ — roughly double the density of concrete-filled counterweights, so the same weight fits in about half the volume. Each unit is weighed before the cover plate is welded on, so the final weight is confirmed, not estimated.
Not sure which you need? Welded fabrication wins on small and medium batches, on short lead times, and on parts still being developed. Casting still wins where envelope space is tight — solid cast iron runs about 7.2 t/m³ against our 4.8 t/m³ filled construction — and on very large volumes where tooling is fully amortised. Tell us your annual quantity and we will tell you honestly which one fits. We supply both.
Built to your drawing, with the mounting, clearances and lifting points machined in. We can also work from a sample or from the machine model alone.
| Application | Reach stackers and other port / container handling equipment |
|---|---|
| Material | Q355B (S355JR) Steel Plate — welded box construction, filled with compacted steel sand at 4.8 t/m³ |
| Weight | Built to your specified weight — no upper size limit. 23,000 kg supplied for a 45 t reach stacker. |
| Weight Tolerance | ±1% of specified weight, confirmed by weighing before the cover plate is welded on |
| Manufacturing | CNC laser cutting → press brake forming → MIG welding → steel sand filling → weighing → cover plate welding → machining → surface finishing |
| Surface Treatment | Shot blasting + anti-rust primer + high-durability enamel paint. Custom RAL colors and logos available. |
| Mounting | Bolt-on with reinforced mounting bosses, machined to your drawing or 3D model |
| Integrated Features | Lifting points, towing eyes, hose and harness clearances machined per drawing |
| Engineering Support | 3D CAD modeling, FEA analysis, reverse engineering from samples |
| Standards | ISO 9001:2015, material cert per GB/T 1591 Q355B (S355JR) |
| Packaging | Heavy-duty wooden crate with VCI rust protection, braced for the part's weight; flat rack or break-bulk arrangement quoted with the part |
| MOQ | 1 unit (sample), 5+ units (production batch) |
| Lead Time | 45 days depending on quantity and customization |
| Customization | OEM/ODM: custom weight, dimensions, color, logo, and mounting arrangement |
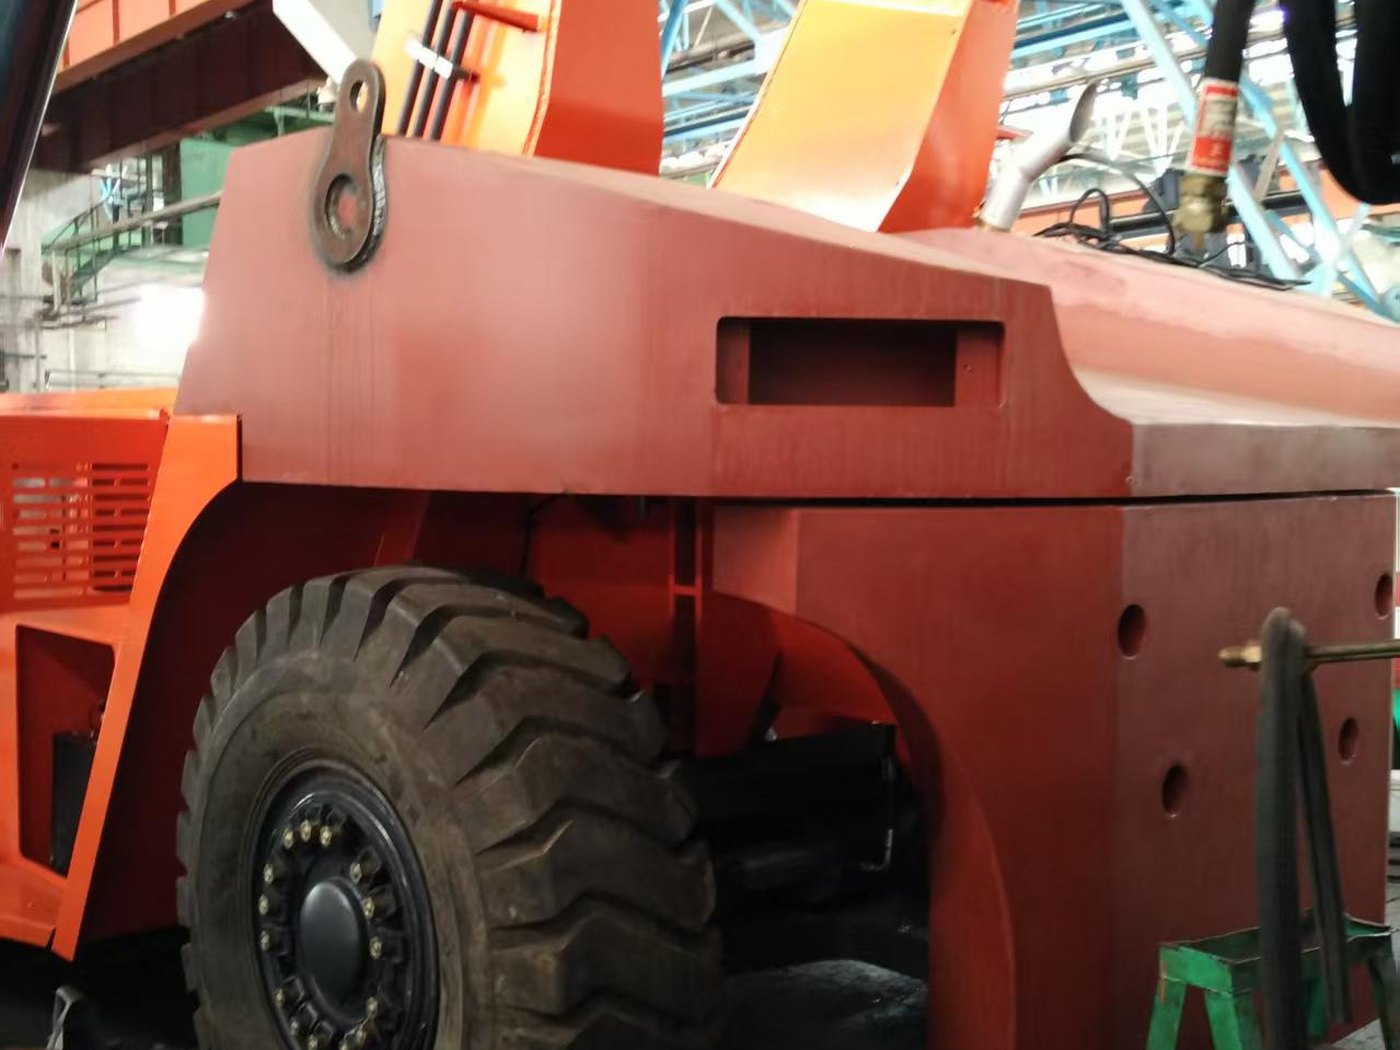
Photographs from our production floor and from customer assembly lines. Each unit is built to the customer's drawing, dimensionally inspected, and weighed before it leaves the factory.
Reach Stacker — Welded Composite Counterweight, fitted
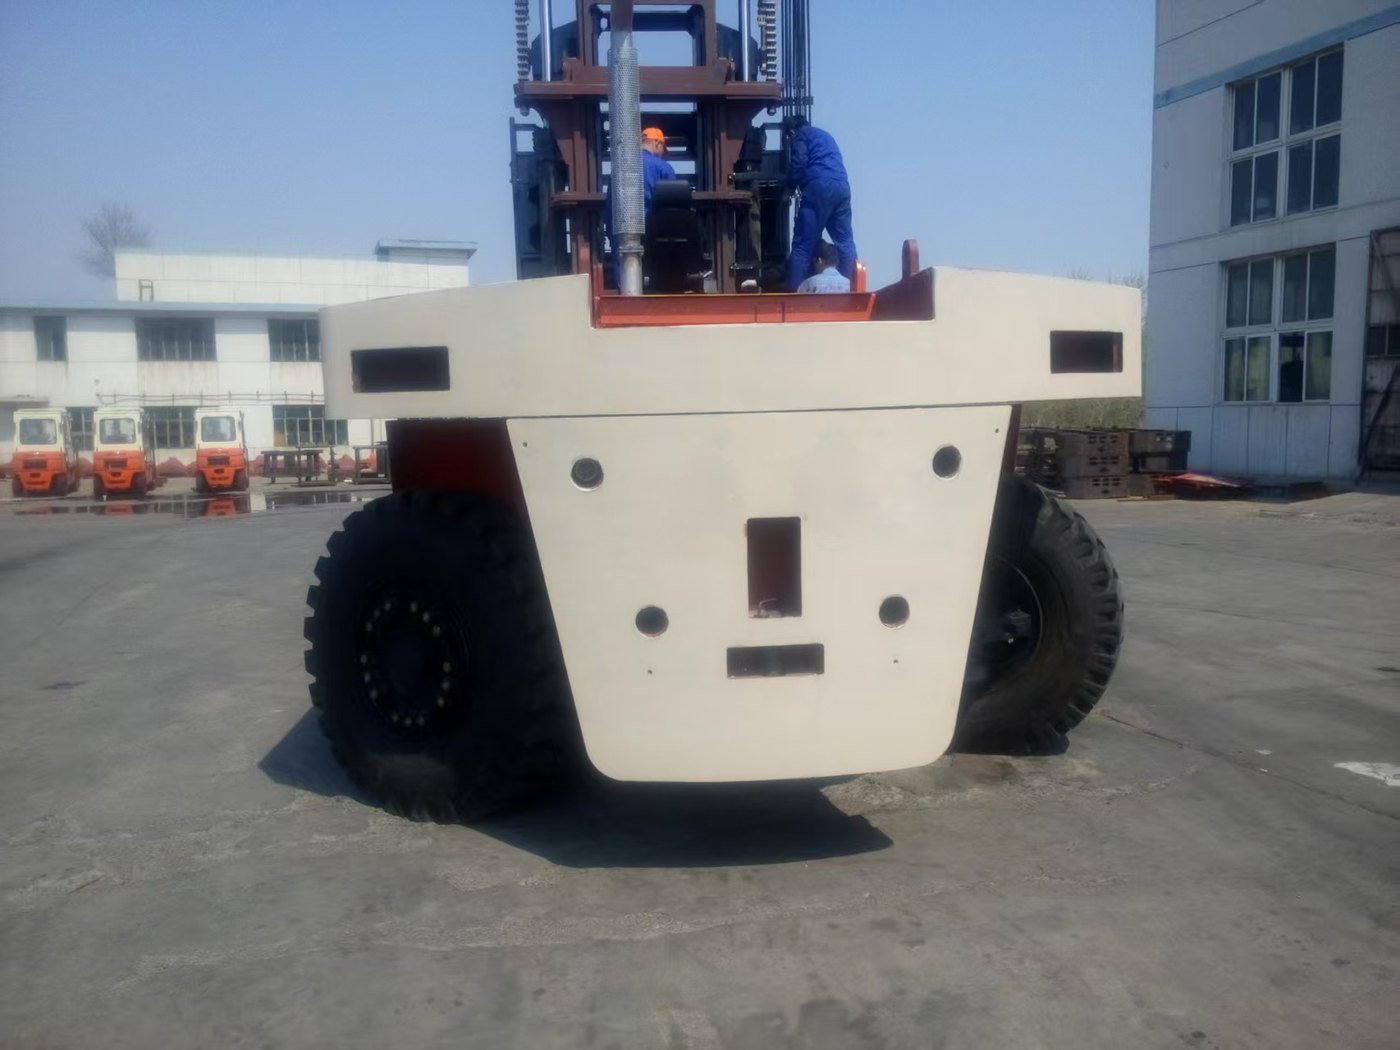 Container Handler — Welded Composite Counterweight, fitted
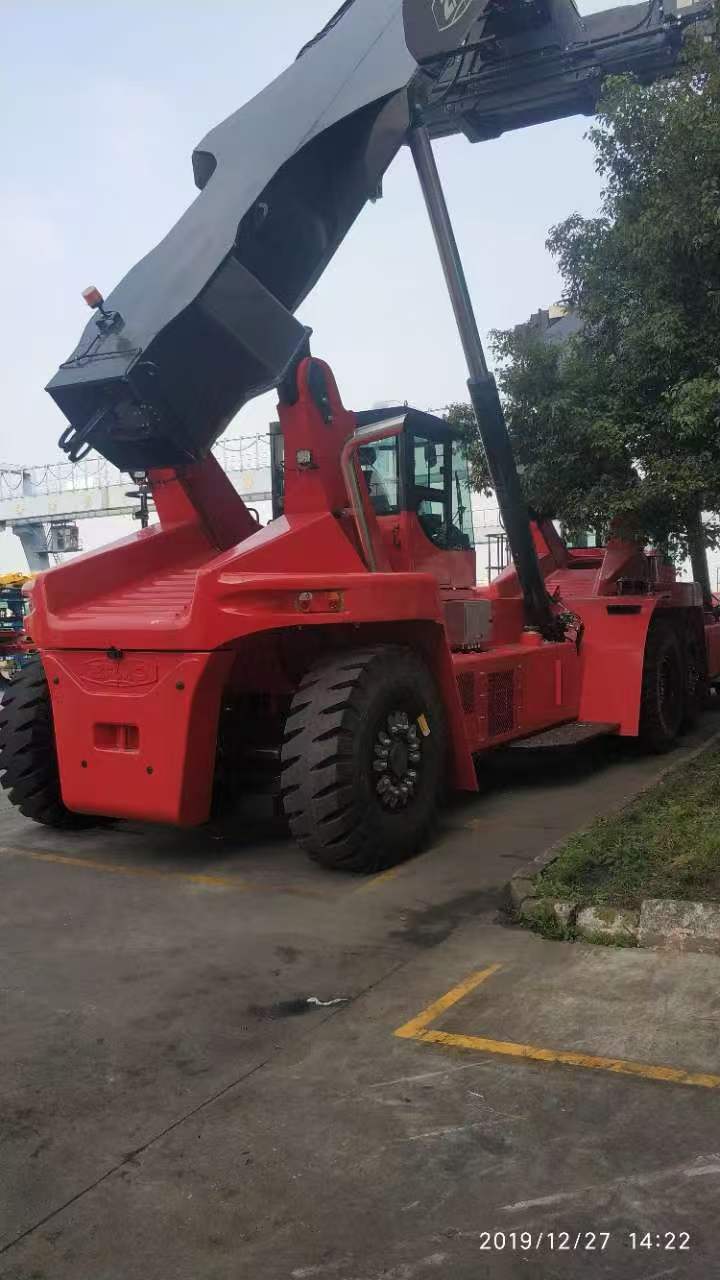 Port Machinery — 45 t Welded Composite Counterweight
On a part this size the drawing does most of the work — and the shipping plan runs a close second.
No drawings? Send us photos or the machine brand and model — our engineers will work from that and send a technical review within 24 hours.
For a 45-tonne reach stacker we build a 23,000 kg counterweight as a welded steel box filled with compacted steel sand. Send us the machine model or your drawing and we will confirm the weight for your machine.
No. Welded fabrication is not limited by pattern, flask or furnace capacity the way a casting is, so there is no upper size limit on a reach stacker counterweight. What we need to plan is the lifting and shipping arrangement for the finished part — tell us the destination port and we will quote the packing and transport with the part.
Yes. Send the existing casting drawing or the part as a sample and we will re-engineer it as a welded fabrication. There is no pattern tooling to pay for, MOQ drops to 1 unit, and a design change is handled by re-issuing the drawing rather than cutting a new pattern. On parts of this size that is usually where the largest saving sits.
Yes. We machine mounting bosses, bolt holes and any local clearances to your drawing or 3D model (STEP/IGES). If you can only supply the machine brand and model, we will work from that and send a technical review within 24 hours.
The hollow box is filled with compacted steel sand at 4.8 t/m³ and the unit is weighed before the cover plate is welded on, so the final weight is confirmed rather than estimated. Standard tolerance is ±1% of specified weight, and the weighing record travels with the shipment.
Standard is Q355B steel plate with compacted steel sand filling for welded counterweights, and cast iron HT200 / ductile iron QT450-10 for cast counterweights. Other steel grades, plating, and galvanizing are available on request.
Yes. Send us the sample or ship it to our facility. Our engineers will measure it, model it in 3D, and confirm the design with you before manufacturing.
Each order includes a material certificate, dimensional inspection report, weight certificate, and packing list. Non-destructive testing (NDT) and certificates of origin are available on request.
Email us your materials → engineering review within 24 hours → technical proposal & quotation → sample/prototype approval → production → 100% inspection → shipment with full documentation.
We reply by email within 24 hours with a technical review and quotation. Attach drawings or photos directly in the email.
Fill out this form and we will reply by email within 24 hours.